When Dual-Standard Compliance Isn’t Optional—It’s Structural
For technical evaluators reviewing materials for international construction projects, galvanized steel sheet for construction isn’t just another component on the bill of materials. It’s a critical interface between design intent, local code enforcement, and long-term asset performance. And when a project spans jurisdictions—say, a mixed-use development in Vietnam using U.S.-designed structural framing, or a logistics hub in Saudi Arabia specifying Chinese-sourced cladding—the question isn’t whether dual-standard compliance is desirable. It’s whether it’s technically feasible without compromising mechanical integrity, coating durability, or process consistency.
ASTM A653 and GB/T 2518 are not parallel specs. They reflect distinct regulatory philosophies, testing priorities, and historical usage patterns. ASTM A653 emphasizes tensile strength consistency, bend test pass/fail thresholds, and zinc mass tolerances tied to service life expectations in North American climates. GB/T 2518 places stronger weight on surface defect classification, adhesion under cold forming, and batch-to-batch uniformity—especially relevant for high-speed roll-forming lines common across ASEAN and Middle Eastern fabrication shops.
Where the Standards Align—and Where They Don’t
Both standards require hot-dip galvanizing with minimum coating masses—but their acceptable ranges differ. ASTM A653 defines coating classes (e.g., G60, G90) based on total zinc mass per side (60 g/m² or 90 g/m²), while GB/T 2518 specifies minimum average coating mass (e.g., Z60, Z120) and permits tighter tolerances on deviation across the sheet width. That means a coil certified to G90 under ASTM may fall short of Z120’s uniformity requirement if edge thinning exceeds 15%—a detail easily missed in pre-shipment documentation but flagged during mill inspection in Shanghai or Guangzhou.
Yield and tensile strength ranges also overlap—but only partially. ASTM A653 Grade 33 (33 ksi ≈ 227 MPa) sits below the lower bound of many GB/T 2518 grades, which commonly start at S220GD (220 MPa min yield). Conversely, GB/T 2518 doesn’t define elongation requirements as stringently as ASTM does for deep-drawing applications. So a sheet passing GB/T 2518’s mechanical tests might still fail ASTM’s mandated 22% minimum elongation after cold bending—critical for roof panel seaming or gutter fabrication.
That’s why “dual-certified” can’t mean “tested once, stamped twice.” It demands coordinated process control—not just final product verification. The zinc-aluminum-copper-magnesium alloy bath composition, line speed, cooling rate, and post-galvanizing tension all influence both coating adhesion and substrate ductility. Adjustments made to satisfy one standard can inadvertently weaken compliance with the other.
How Real-World Production Bridges the Gap
At Hongteng Fengda, dual-standard alignment starts before the coil enters the galvanizing line. We calibrate base steel chemistry—particularly carbon, manganese, and silicon—to meet the combined yield/tensile/elongation envelope required by both ASTM A653 and GB/T 2518. For example, DX53D and S320GD grades are routinely selected for cross-market projects because their balanced microstructure delivers ≥240 MPa yield strength *and* ≥22% elongation without sacrificing formability.
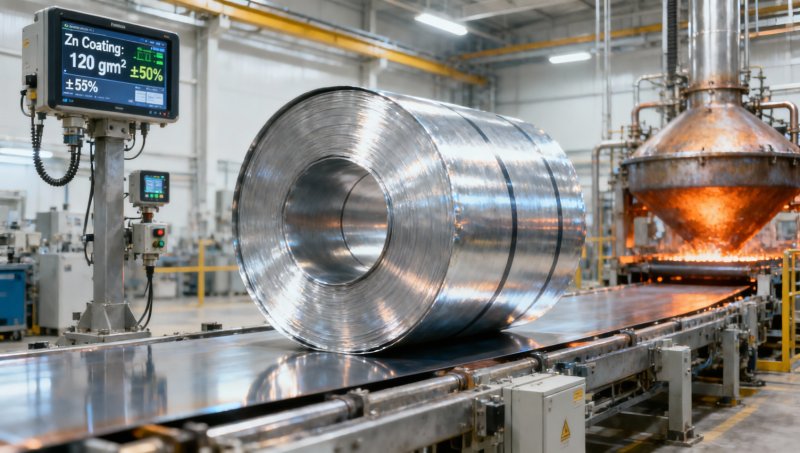
Coating mass is controlled in real time via electromagnetic gauging, with automatic bath temperature and immersion time adjustments to maintain 60–275 g/m² across full-width tolerance bands—not just average values. Surface quality is assessed under calibrated lighting and magnification, referencing both ASTM’s visual grading scale and GB/T 2518’s defect size/type matrix. Third-party labs verify results against both standards—separately, not concurrently—because inter-lab correlation isn’t assumed.
This level of control matters most when specifications intersect with application reality. A warehouse roof in Dubai needs corrosion resistance against saline aerosols *and* must survive roll-forming into trapezoidal profiles without flaking. A prefabricated school building in Ontario requires consistent weldability *and* must pass fire-rated assembly testing where zinc vaporization behavior is part of the assessment. Neither scenario allows for “close enough.”
What Technical Evaluators Should Verify—Beyond the Certificate
A dual-standard certificate is necessary—but insufficient. Here’s what to request before approving material submittals:
- Mill test reports showing *individual* ASTM A653 and GB/T 2518 test results—not a merged summary
- Zinc coating distribution data across width and length (not just average g/m²)
- Batch-specific chemical composition reports confirming Si/Mn ratios within dual-compliance windows
- Evidence of bend testing per ASTM A653 Section 9 *and* GB/T 2518 Annex B (different mandrel diameters, different pass criteria)
Thickness tolerance is another quiet divergence. ASTM A653 permits ±0.005 in (≈0.13 mm) for 0.8 mm base metal; GB/T 2518 allows only ±0.08 mm for the same thickness. That 0.05 mm gap affects load calculations in lightweight steel framing—especially when paired with cold-formed sections from the same supplier.
Not All Galvanized Sheets Are Built for This Level of Scrutiny
Many producers optimize for one market—then retrofit documentation for the other. That often shows up in inconsistent zinc layer adhesion on cut edges, marginal elongation margins, or narrow width availability (e.g., only 1000 mm coils, limiting panel layout efficiency in European projects). At Hongteng Fengda, we support custom widths from 600 mm to 1500 mm and lengths from 1 m to 12 m—not as an upsell, but because dimensional flexibility reduces waste and rework downstream. Our Galvanized Steel Sheet is produced across a spectrum of grades—including SGCC, DX54D, S350GD, and S550GD—each validated against both ASTM and GB test protocols before release.
We don’t treat dual-standard compliance as a checkbox. It’s a continuous calibration loop—between metallurgy, process engineering, and field feedback from projects across North America, Europe, and Southeast Asia. If your next tender includes references to both ASTM A653 and GB/T 2518, confirm whether the supplier has run concurrent validation—not just sequential testing. And ask how they handle discrepancies when test results sit near the boundary of either spec. That’s where real capability reveals itself.
Please give us a message


Please enter what you want to find