A lower price per piece can become the more expensive purchase when perforated steel angle reaches the cutting bench. Stock bars may need end trimming, a hole pattern may not match the assembly, or leftover sections may be too short for the next part. For buyers sourcing angulo agujereado, the useful comparison is total procurement and conversion cost divided by accepted finished length, not the quoted price divided by nominal stock length.
Start by giving each supplier the same finished-part schedule, hole requirements, and delivery basis. Then calculate how many compliant parts each proposed stock length can produce after trimming and cutting losses. This exposes offers that look inexpensive but require additional bars, extra drilling, or more workshop time.
Define usable length before comparing prices
“Usable length” needs a shared definition. A supplier may use it to describe the straight section remaining after damaged ends are removed. Your workshop may mean the total length of finished pieces that satisfy the drawing. Those are different quantities, and only the second measures yield against a specific order.
For quote comparison, use accepted finished meters: the sum of the lengths of parts that meet the required dimensions, hole locations, material specification, and finish. A remnant that could theoretically be used someday should not count as accepted finished output for the current job.
The basic calculation is:
Cost per usable meter = total attributable cost ÷ total accepted finished meters.
Total attributable cost should include the purchased material, delivery to the agreed location, and the processing needed to make the parts acceptable. Keep recoverable scrap value separate until there is a defensible basis for it. Otherwise, an optimistic scrap allowance can conceal poor cutting yield.
Cost per usable meter is a normalization tool, not permission to compare unlike products. Different leg sizes, thicknesses, grades, or hole layouts must first pass the same technical requirements. A lighter angle is not a saving if it fails the specified duty.
Give suppliers a cutting schedule, not just a total meter requirement
A request for a total quantity of perforated angle leaves suppliers free to quote different stock lengths. That may be useful commercially, but it does not show whether those lengths fit your production plan. Include a schedule of finished lengths and quantities so each offer can be evaluated against the actual demand.
Ask suppliers to identify any assumptions rather than silently substitute their standard perforation pattern. A quote described only as “standard punched angle” is not sufficiently defined when the assembly depends on a particular hole-to-end distance.
Check the hole pattern before optimizing the cuts
Plain angle can often be nested around finished lengths and saw kerf alone. Perforated angle introduces another constraint: the location of each cut relative to the holes. A bar can contain enough nominal length while still failing to yield the required parts.
The important dimension is not just hole pitch. It is also pattern phase, meaning where the repeating pattern begins relative to the stock end. Two bars with identical hole spacing can produce different results if their first holes sit at different distances from the end.
Confirm whether finished ends must fall between holes, whether slots may be intersected by a cut, and whether the first and last connections have specified edge distances. Do not assume that shifting a cut to preserve a hole is acceptable: the shift may put the finished part outside its length tolerance.
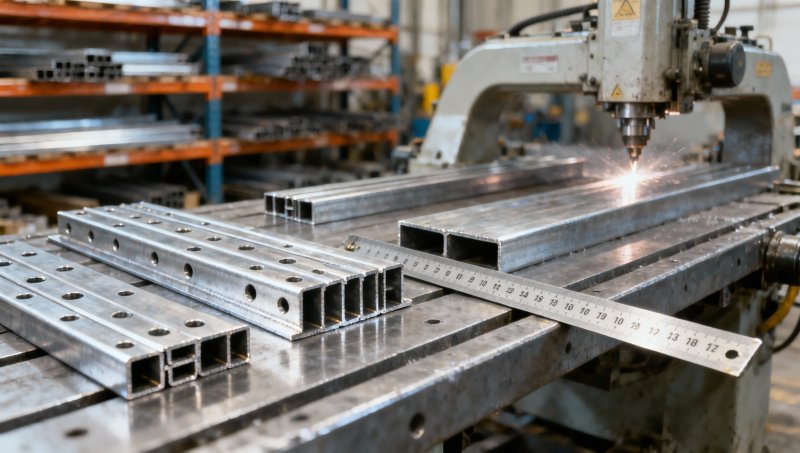
A dimensioned drawing showing the stock end, first hole, repeating pitch, and proposed cut positions is more useful than a general product photograph. Where holes occur on both legs, the drawing should show their relative alignment as well. An offset between rows may affect bracket positioning even when the overall pitch appears correct.
Additional drilling is not automatically a practical remedy. It adds labor and may affect edge distances, coating continuity, or the suitability of the connection. For load-bearing applications, any changed hole layout should be checked against the approved design before its cost is treated as an acceptable conversion option.
Build the yield calculation around complete parts
Calculate yield separately for each offered stock length. First deduct unavoidable end preparation from the minimum guaranteed supplied length. Then nest the required parts using the actual cutting process and verified hole-position constraints.
A proposed cutting layout is feasible only when:
Sum of finished part lengths + actual kerf losses + required end trims ≤ available stock length.
The number of kerf losses depends on the cutting sequence. Do not automatically multiply every part by the blade width: a usable existing end may avoid a cut, while end squaring or separating a remnant may add one. Have the workshop confirm the assumed process.
- Use the guaranteed lower length limit. A nominal stock length may be supplied short within its agreed tolerance. A layout that fits only the nominal dimension is fragile.
- Apply end trimming consistently. Include trimming required for squareness, damage removal, or hole-position alignment. Avoid deducting the same trim twice.
- Nest the complete order. Mixing long and short parts can improve yield, but the output must match the required quantities rather than generate surplus short pieces.
- Record remnants separately. Identify their lengths and hole conditions, then decide whether they match another confirmed requirement.
For a repeated part length, dividing available stock length by finished length is only a preliminary check. The final number of parts must account for kerf, end conditions, and hole alignment. For mixed lengths, use a cutting spreadsheet or nesting tool that can represent those constraints; a length-only optimizer may overstate usable output.
Once the layout is validated, calculate the bars needed to complete the schedule. Apply minimum order quantities, bundle multiples, and any agreed spare allowance afterward. Excess purchased bars still belong in the cost numerator unless they are allocated to another approved requirement.
Put freight, finishing, and workshop costs on the same basis
Longer stock can reduce cutting waste but increase logistics or handling costs. Check whether the proposed length fits the planned transport, unloading equipment, storage racks, and cutting line. A high-yield bar is not necessarily economical if it requires a different shipping arrangement or an additional handling operation.
Compare delivery terms and named places explicitly. An ex-works offer and a delivered offer cannot be ranked fairly until their respective freight, loading, insurance where applicable, customs-related costs, and inland delivery charges have been reconciled. Use current quotations for these items rather than unsupported estimates.
Finishing also changes the conversion route. Pre-coated stock may need treatment at cut ends or newly drilled holes. Material finished after cutting may involve different handling, batch charges, or lead times. Agree the required finish and repair method before assigning costs; coating descriptions without measurable requirements are difficult to compare.
A practical comparison sheet should keep these items visible:
- Purchased bars, quoted unit price, and total material cost.
- Freight, packaging charges, and delivery-related costs not included in the offer.
- Cutting, deburring, permitted drilling, and required finishing costs.
- Inspection costs and any order-specific setup charges.
- Accepted finished meters, with surplus stock and remnants shown separately.
Keep uncertain costs marked as pending rather than treating them as zero. If a supplier has not confirmed end tolerances or packaging dimensions, the resulting yield or freight figure is provisional. That uncertainty may be enough to delay a purchasing decision.
Separate usable remnants from optimistic inventory credits
A leftover section has value only when there is a credible route to using or selling it. Its length alone is insufficient: the hole pattern, end condition, grade, and finish must also fit the future requirement.
For repeat production, an identified remnant can be assigned to a scheduled part and tracked in inventory. For a one-off order, it is usually clearer to charge the full purchase to the job and show any potential recovery separately. This avoids favoring a supplier simply because its cutting plan leaves more unallocated stock.
Scrap proceeds should likewise reflect the recoverable material and applicable handling costs. Do not value punched angle using the mass of an unperforated section without checking the removed material. If suppliers quote by weight, request the basis of invoicing and the expected piece count so the offer can still be converted to cost per accepted finished meter.
Resolve specification conflicts before awarding the order
Quotes sometimes arrive with related catalog items or mixed descriptions. Keep those lines outside the perforated-angle comparison unless they satisfy the same drawing and material requirements. A square bar, for example, may belong elsewhere in the assembly but is not a substitute for a perforated angle.
The listing for 310 Stainless Square steel rod illustrates a specification issue worth resolving: its title refers to 310, while the supplied material information identifies 201 stainless steel. Its stated length range is one to six meters, with customization available, but neither the title nor that length range establishes suitability for the angle requirement. If this item is needed elsewhere in the bill of materials, obtain a confirmed grade and dimensional specification and evaluate it on a separate line.
For the perforated angle itself, request an approved drawing, agreed tolerances, and relevant material documentation. A general reference to ASTM, EN, JIS, or GB does not identify the exact product or grade requirement. The purchase order should state the applicable specification rather than rely on a broad catalog claim.
Before release, ask the selected supplier to confirm the proposed stock lengths and perforation arrangement against the cutting schedule. Where yield depends closely on hole phase or end tolerance, verify a first article or representative sample before committing to the full processing run.
The award record should show both cost per accepted finished meter and total cost to complete the required schedule. Choose the lower evaluated cost only after the offer passes the technical checks and its yield assumptions are supported. If a small quoted saving depends on unconfirmed lengths, undocumented hole positions, or speculative remnant reuse, keep that saving provisional rather than building it into the purchasing budget.
Please give us a message


Please enter what you want to find