How to Select the Right Galvanized Steel Channel for Outdoor Structural Projects
Selecting the right galvanized steel channel for outdoor structural projects isn’t about matching a catalog number to a drawing—it’s about aligning material behavior with real-world exposure, load path integrity, and long-term maintenance constraints. For project managers overseeing infrastructure in coastal zones, high-humidity industrial sites, or regions with aggressive de-icing salt use, the choice of galvanized channel directly determines whether corrosion initiates at weld seams, accelerates at cut edges, or propagates beneath mechanical fasteners—issues that rarely appear in shop drawings but routinely surface during commissioning or 3–5-year inspections.
The core decision hinges on three interdependent variables: zinc coating mass and uniformity, base steel grade and tensile response under sustained loading, and dimensional tolerance control across length and flange geometry. These are not abstract specs—they define how the channel resists localized pitting when exposed to chloride-laden air, maintains stiffness under wind-induced cyclic loads, and interfaces reliably with bolted connections without requiring field reaming or shimming.
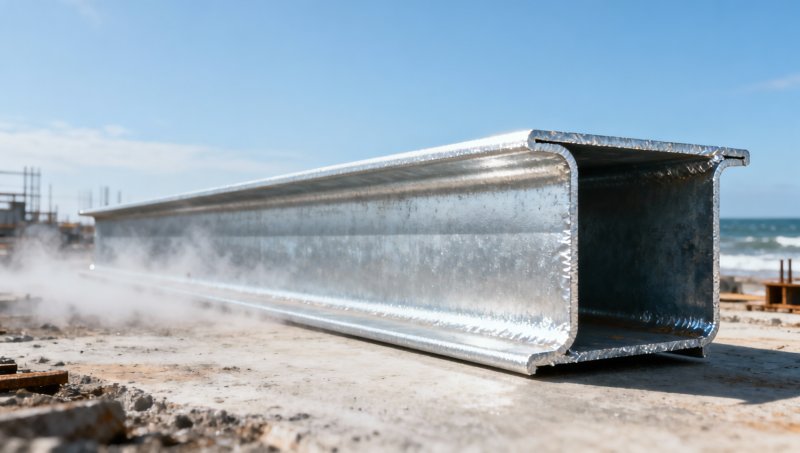
Zinc coating is the first line of defense—but thickness alone misleads. A nominal 60 μm coating applied via hot-dip galvanizing must be verified across all surfaces: inside the web-to-flange radius, along cut ends, and at drilled holes. ASTM A123 and EN ISO 1461 specify minimum average coating masses (e.g., 610 g/m² for steel >6 mm thick), but they do not guarantee coverage continuity at geometric discontinuities. In practice, channels with tight internal radii (<3 mm) often show reduced zinc adhesion in the corner region—especially if cold-formed prior to galvanizing. That’s why mill-tested, pre-galvanized channels—where forming occurs after coating—deliver more predictable performance in exposed structural framing, even if unit cost rises 8–12%.
Base steel selection matters beyond yield strength. Q235B and S235JR offer adequate ductility for general bracing, but their lower tensile-to-yield ratio (~1.3–1.4) limits reserve capacity under unexpected overloads. For cantilevered signage supports or rooftop solar racking in typhoon-prone areas, S335JR or ASTM A572 Grade 50 provide higher strain hardening and better post-yield energy absorption—critical when wind gusts exceed design basis assumptions. Importantly, these grades maintain consistent galvanizing response: no excessive dross formation, minimal spangle variation, and reliable coating adherence through thermal cycling.
Dimensional precision affects more than fit-up. Flange width tolerance ±2 mm may seem minor—until you’re bolting into pre-drilled base plates or nesting channels into welded truss nodes. Excessive variation forces field grinding or oversized washers, both of which compromise corrosion protection at connection points. Likewise, web thickness deviation beyond ±0.02 mm alters section modulus calculations—notably for channels used as secondary beams carrying distributed live loads. A 5% reduction in effective web thickness can shift deflection from acceptable (L/360) to borderline (L/280), triggering re-analysis or costly reinforcement.
Cut-edge corrosion remains the most underestimated failure mode. Even with 60+ μm zinc, freshly cut ends expose bare steel. Without proper edge sealing—either via touch-up zinc-rich paint or mechanical encapsulation—the galvanic cell forms rapidly in humid conditions, undercutting adjacent coated areas. This isn’t theoretical: field audits of 12-year-old coastal walkway structures show 70% of premature section loss originating within 25 mm of unsealed cut ends—not at mid-span or weld zones. The solution isn’t thicker coating; it’s specifying channels with pre-cut, factory-sealed ends or mandating certified edge treatment protocols in procurement specs.
Load-path compatibility is frequently overlooked. Galvanized channels used in moment-resisting connections require controlled bolt hole spacing and flange stiffness. If the flange flexes excessively under bolt pretension—common with thinner-gauge or wide-flange variants—the clamped interface slips before full friction develops, reducing joint rotational stiffness by up to 40%. That shifts load distribution in multi-bay frames, increasing demand on adjacent members. Project managers should verify bolt group layout against actual flange moment of inertia—not just nominal dimensions—and reject suppliers who quote only “standard EN 10029 tolerances” without confirming flange flatness (≤1 mm per meter) and parallelism (≤0.5 mm across width).
 Material traceability matters less for compliance paperwork and more for forensic accountability. When a galvanized channel fails prematurely, root cause analysis depends on verifiable batch-level data: melt chemistry (particularly Si and P content, which affect zinc alloy layer formation), tensile test reports tied to specific coil IDs, and galvanizing bath temperature logs. Suppliers offering only generic mill certificates—not lot-specific test reports—shift diagnostic risk onto the project team. Hongteng Fengda provides batch-level zinc coating mass verification (via magnetic induction + cross-section metallography) and base steel tensile data traceable to furnace heat numbers—enabling direct correlation between lab results and delivered sections.
For applications demanding both structural integrity and surface functionality—such as pedestrian ramps, equipment platforms, or marine access grating—235JR Patterned steel plate offers an integrated alternative where anti-slip performance and bending resistance coexist with galvanizing compatibility. Its patterned surface eliminates secondary skid-resistant coatings while maintaining consistent zinc adhesion across raised features—provided pattern depth adheres to the 0.2× substrate thickness rule specified in EN 10147.
Ultimately, selecting the right galvanized steel channel means rejecting “off-the-shelf” assumptions. It requires verifying coating mass *at critical geometries*, confirming base steel grade suitability *for the actual loading regime* (not just code-minimum), and treating dimensional tolerances as functional requirements—not manufacturing allowances. Projects that treat galvanized channel as a commodity item pay later in inspection delays, unplanned maintenance, or premature replacement. Those that anchor selection in exposure-specific performance logic—rather than catalog price or lead time—achieve decades of service without hidden lifecycle costs.
Previous page: Already the first one
Next page: Already the last one
Please give us a message


Please enter what you want to find